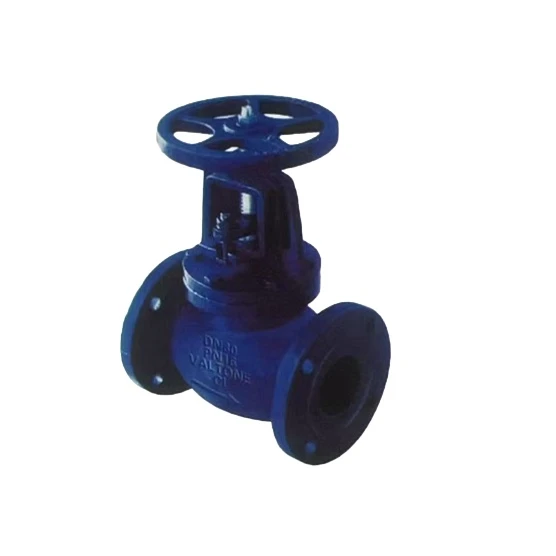
Industrial pipeline systems require stable and precise flow regulation equipment to ensure long-term, safe, and efficient operation in complex working environments. As a core flow control component, the globe valve has become one of the most widely used industrial valves in chemical, petrochemical, power, and thermal pipeline systems due to its reliable throttling performance, flexible structural design, and strong environmental adaptability.
A standard globe valve features a classic spherical valve body structure, composed of a movable disc and a fixed seat. This mature mechanical structure enables accurate flow adjustment and reliable medium cut-off, effectively solving unstable flow control and pipeline pressure fluctuation problems in industrial production. To adapt to the increasingly harsh working conditions of modern industrial pipelines, the optimized new-generation globe valve series has achieved comprehensive upgrades in structural design, manufacturing materials, and sealing technology.
In terms of structural design, the product provides two mainstream types: standard straight-through structure and straight-through bellows structure. The standard straight-through type is suitable for conventional industrial pipeline regulation and cut-off scenarios, while the bellows type effectively improves operational stability and sealing safety under frequent opening and closing cycles, meeting high-standard industrial working conditions.
To match different media characteristics, pressure levels and temperature environments, the globe valve is equipped with a wealth of high-quality valve body material options, including 304, 316 and 316L stainless steel, WCB carbon steel, A105 forging steel, and ZG20CrMoV high-temperature alloy steel. Diversified material configurations enable the valve to resist corrosion, high temperature and high pressure, adapting to various complex medium environments such as water, steam, oil and chemical fluids.
In terms of installation and operation flexibility, the product supports flanged and welded mainstream connection methods, which are convenient for on-site installation, fixing and later maintenance. Meanwhile, it covers multiple actuation modes including manual, electric, pneumatic and hydraulic types, which can be freely matched according to automated pipeline system requirements, realizing precise remote and on-site flow control.
The valve boasts a wide range of pressure and temperature resistance. The conventional nominal pressure ranges from PN 1.6–16 MPa and Class 150–1500 lb. For ultra-high-pressure industrial scenarios, the customized high-specification model can reach PN 16–420 MPa and Class 150–2500 lb. Its operating temperature ranges from -29°C low temperature to 648°C ultra-high temperature, fully covering most extreme industrial pipeline working conditions.
In terms of core performance and structural advantages, the upgraded globe valve has excellent wear resistance and sealing stability. The sealing surfaces of the valve body and disc adopt hard-alloy overlay technology, which greatly enhances abrasion resistance and corrosion resistance, extending the service life of the valve under long-term cyclic operation. The valve stem is equipped with a professional compensation mechanism, which can automatically adjust the fitting accuracy of the sealing surface to avoid sealing gaps caused by mechanical wear.
In addition, the bonnet cavity adopts a self-tightening sealing structure. Its unique structural design enables the sealing performance to be continuously improved with the increase of pipeline pressure, realizing zero leakage under high-pressure working conditions. Equipped with high-temperature and wear-resistant packing materials, the valve maintains stable sealing performance for a long time under high-temperature and frequent opening and closing conditions, effectively reducing pipeline maintenance costs and improving the overall operational safety of industrial systems.
With comprehensive performance advantages in structural diversity, material reliability, wide temperature and pressure adaptability, and superior sealing technology, the optimized globe valve provides stable and long-lasting flow control solutions for global industrial pipeline systems, and has become a preferred choice for high-end industrial fluid control projects.